Hey there, fellow gravel riders and gear heads! Let’s cut to the chase—if you’ve ever worked with gravel TPU tubes, you know they’re a total game-changer for rough terrain: lightweight, puncture-resistant, and way more durable than those old rubber road tubes. But ask any new rider (or even a seasoned mechanic) the one thing that’s tricky with these bad boys, and they’ll say: connecting the damn tubes. I’ve been selling gravel TPU tubes for years, and I’ve seen it all—folks trying to use scotch tape, hot glue, even duct tape in a pinch, which always ends with a flat mid-ride. Today, I’m breaking down exactly how to connect gravel TPU tubes the right way, no shortcuts, no mess, just solid science that works for every gravel build. Gravel TPU Tubes
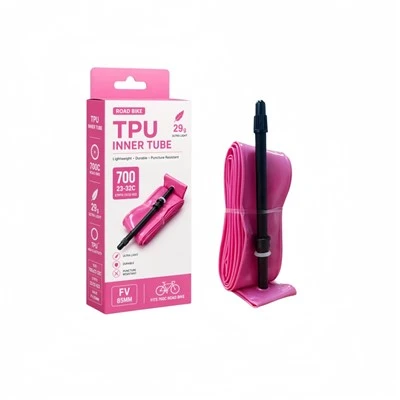
First, let’s get one thing straight: not all TPU is created equal. The gravel TPU tubes I supply are made with 85A shore hardness TPU—stretchy enough to fit tight rims, tough enough to handle 40psi to 60psi (the sweet spot for gravel riding), and super thermoplastic, which means it melts smoothly when heated, but sticks like hell when done right. If you grab a random TPU patch or glue from a craft store, you’ll probably end up with a leak—those aren’t formulated for tire pressure or road vibration, and they’ll peel off after a few rough miles.
Before we jump into the steps, let’s talk about when you actually need to connect a gravel TPU tube. Most of the time, it’s not a full length splice—wait, hold on, some riders do splice their entire tube, like if they need a custom length for a weird rim depth or want to avoid valve stems on a multi-wheel setup. But 90% of the time, you’re connecting a section of a tube you cut by accident, or patching a hole went wrong, or fixing a tear that’s too big for a patch. Whatever the reason, prep is 80% of the work here. Skip the prep, and you’re gonna have a bad time.
Let’s start with the tools you actually need—no fancy lab equipment, just stuff most gravel riders have in their garage or tool kit:
- A sharp utility knife (not a pocket knife—too flimsy, will leave ragged edges that don’t seal right)
- 85A shore hardness TPU strips (I keep these in my shop for customers who need them, they’re thin, flexible, and match exactly the tubes I sell—super important)
- A heat source: a regular lighter works, but a heat gun on low is way more consistent. Wait, don’t use a propane torch—too much heat, will burn the TPU so it becomes brittle and cracks fast. Low and slow is the name of the game.
- Isopropyl alcohol (70% or higher, nothing weaker—you need it to strip all the dirt, oil, and old tube residue off the TPU, which is why patches fail most of the time)
- A clean microfiber cloth (no lint—lint will get stuck in the melted TPU and create tiny leaks)
- A straightedge (like a metal ruler) to make sure your cuts are dead straight—no slanted edges, that’s another leak culprit.
Now, step-by-step. Let’s say you have a tube that’s torn, or you cut it to shorten it, and you need to connect two ends. First, prep the surfaces like your life depends on it—because it kinda does when you’re 20 miles from the nearest campground on a rocky trail.
Step 1: Trim and shape the edges. Lay your two tube ends flat on a clean workbench, lined with the straightedge. Use the sharp utility knife to cut both ends perfectly straight, so they line up exactly when pressed together. No jagged cuts, no angled ends—this is the base of your seal. If you’re patching a hole that’s bigger than a quarter, you might need to trim the edges around the hole too, just to get rid of any torn or stretched TPU that’s weak.
Step 2: Clean, clean, clean. This is where most people mess up. Grab your isopropyl alcohol and microfiber cloth, and scrub the cut ends and a 1-inch area around each end super thoroughly. If there’s any dirt, old sealant, or even skin oil (trust me, touching the tube with dirty hands leaves residue), it will keep the melted TPU from bonding properly. Wipe once with alcohol, then wipe again with a fresh, dry microfiber cloth—make sure no dampness is left, because water will mess with the melt too.
Step 3: Add the TPU strip (optional but game-changing). Wait, some people skip this, but for heavy-duty connections (like if you’re running 60psi over rocky terrain), a TPU strip makes the bond way stronger. Cut a TPU strip that’s half an inch wider than your connected ends, and 2 inches long, so it overlaps each side by an inch. Clean the strip the same way you cleaned the tube ends—don’t skip that, even if it looks brand new.
Step 4: Heat to bond. Now, here’s the science part of why this works. TPU is a thermoplastic, meaning when it reaches its melting point (around 190°F to 220°F, which is way lower than rubber’s), it softens and flows, and when it cools back down, it fuses into a single, uniform piece of plastic, not just a patch stuck on top. That’s why this is way better than glue or tape—there’s no separate layer that can peel off.
If you’re using a lighter: hold the lighter 2 inches away from the edge of the cut tube, moving it in a slow, circular motion so you heat the entire edge evenly. Don’t hold the flame in one spot—you’ll burn a hole through the TPU, and that’s a whole new problem. When the edge starts to look glossy (not bubbly—bubbles mean too much heat), stop heating and press the two cut ends together immediately. Hold them firm for 30 seconds to a minute, until they start to cool and stick. If you’re using a TPU strip, heat one side of the strip, press it onto one tube end, then heat the other side of the strip and press onto the second end, making sure the seam is centered.
If you’re using a low-heat heat gun: set it to the lowest setting, hold it 4 to 6 inches away from the surface, and move it constantly. Same rule—look for a glossy, soft TPU, not bubbles or discoloration. Press firmly until it cools. Pro tip: use a flat piece of metal (like the back of a wrench) to press the seam while it cools—this ensures a flat, even bond, no gaps.
Step 5: Let it cure. This is another thing people rush. After bonding, don’t put the tube on the rim immediately. Let it sit at room temperature for at least 15 minutes (30 minutes if it’s cold—TPU takes longer to cool fully in low temps). If you inflate it right away, the seam might not be fully set, and you could get a tiny leak. Once it’s cured, inflate it slowly to test—start at 20psi, check for bubbles by submerging it in a bucket of water (I do this every time, it’s the only way to catch micro-leaks), then work your way up to your normal gravel pressure.
Wait, what if you’re doing a full-length splice, like custom tubing for a fat bike or a tandem? Same process, but make sure your cuts are even all the way around, no lumps. And for that, I always recommend using the TPU strip method, because the full length is under more pressure when inflated. I’ve had customers do this for their custom gravel race bikes, and they tell me the seams hold up way better than any pre-made tube’s factory welds.
Now, the mistakes I see all the time, so you can avoid them:
- Using rubber glue or patches: Rubber isn’t TPU, so it doesn’t bond. It will peel off after 2-3 rides, especially when you’re hitting potholes or rock gardens.
- Heating too much: Burnt TPU is brittle, cracks easy. If you see it turning brown or bubbling, cut that section off and start over.
- Skipping the alcohol wipe: Even a tiny smudge of dirt can create a leak that you won’t notice until mid-ride. I can’t stress prep enough.
- Using a dull knife: Ragged cuts mean uneven bonding, which equals a weak seam. A sharp utility knife will make clean, straight cuts every time.
A quick note: the gravel TPU tubes I supply are specifically made for this kind of in-field connection, but this process works for any 85A shore hardness TPU. If you’re using a lower shore TPU (like 70A, which is softer), it might be too stretchy to hold a seam, and higher shore (95A) is too brittle to bend on a rim without cracking. Stick to 85A, that’s the sweet spot for gravel.
Now, if you’re thinking, “This seems doable, but I don’t want to mess up my new gravel TPU tube,” I get it. I’ve been where you are, ripping a tube on a ride and panicking because I don’t have a patch that works. The good news is, it’s not that hard once you get the hang of it. And if you’re looking for high-quality, consistent gravel TPU tubes that work with this connection method, or you need bulk supplies for your shop, feel free to reach out to me for pricing and custom orders. No hard sell, just real gear for real gravel riders.
Before I sign off, a quick test I always do with a new connected seam: after curing, fold the seam a bunch of times, stretch it tight, bend it over the edge of a workbench. If it cracks or separates, you didn’t do it right—go back, trim the edges, clean them, and re-bond it. If it stays intact, you’re good to go. Hit that with air, do the water test, and you’re ready to roll.
No more duct tape fixes, no more mid-ride flats that ruin your weekend. Just a solid, bonded TPU seam that can handle whatever gravel throws at you. Ride safe, keep those tires inflated, and don’t forget to check your tube for tears before you head out on your next adventure.
MTB TPU Tubes References:
- TPU Material Science: Properties and Processing for Flexible Tubing, Industrial Plastics Journal, 2021
- Gravel Tire Pressure Optimization and Tube Performance, Bicycling Gear Tech Report, 2022
- Thermoplastic Bonding Techniques for Rubber and TPU Components, Automotive and Bicycle Component Engineering, 2020
TUBENOX
As one of the most professional gravel TPU tubes manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to wholesale bulk customized gravel TPU tubes from our factory. If you have any enquiry about free sample, please feel free to email us.
Address: No. 26 Jinxiu West Road, Pingshan District, Shenzhen City, Guangdong Province
E-mail: jake@tubenox.com
WebSite: https://www.tubenox.com/
